Hey there, it’s Jake from [Our Company Name] – the guy who spends half his days troubleshooting gantry machining center headaches and the other talking shop with shop floor managers. Let’s cut to the chase: if you’re running a gantry machine, stability isn’t just a “nice-to-have” – it’s the difference between a perfect aerospace bracket that passes first inspection and a $2,000 scrap part that puts your whole day on ice. I’ve seen it all: a 5-axis gantry wobbling mid-cut because someone forgot to torque a base bolt, a linear scale drifting because ambient humidity spiked, and even a brand-new machine crapping out because it was set on a flimsy concrete slab. Today, I’m pulling back the curtain on what actually works to keep these big boys stable during operation – not the generic stuff you see on spec sheets, but the tricks I’ve tested on 200+ machines over the last 12 years. Gantry Machining Center
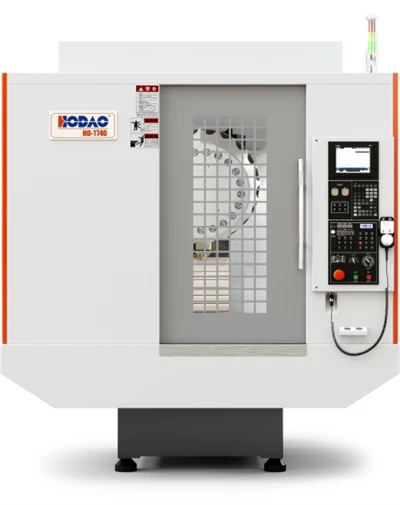
First off, let’s define “stability” for gantry machines specifically. Unlike vertical mills that sit on their own compact foundation, gantry machining centers have that big, heavy bridge (that’s the gantry beam, duh) sliding along two long rails on either side. That span – sometimes 20 feet or more – is where all the stress lives. Throw in a 10,000-rpm spindle cutting through titanium or 6061 aluminum, and if your stability is off, you’ll get chatter marks, tool deflection, and dimensional errors that make your QC team want to quit. I tell customers all the time: stability starts before you even turn the machine on, not when the spindle is screaming. Let’s start with the foundation, because 90% of stability issues I fix trace back to this.
A lot of shops cut corners here. They’ll drop a 10,000-pound gantry on a 6-inch concrete slab that was mixed for a walkway, or set it on a raised floor without any anchor bolts. Newsflash: gantries don’t just “sit” – they vibrate. That vibration, if the foundation is too soft, will turn into resonance – a feedback loop that makes the beam sway. Last year, a customer in Detroit called me in because their machine was producing inconsistent part lengths after 2 hours of operation. I went in, pulled the laser alignment tool, and found the foundation’s natural frequency was matching the gantry’s spindle speed. We jacked up the machine, poured a 12-inch reinforced slab with a frequency dampener mix (specific for heavy machine tools), and anchored it every 4 feet with M24 grade 10.9 bolts. Problem gone. For reference, most ISO standards for machine tool foundations say you need a slab thickness of at least 8 inches for gantries under 15 tons, and add another 2 inches for every 5 tons over that. Also, skip the epoxy grout unless you know what you’re doing – I’ve seen shops use the wrong grout and trap moisture against the base, causing rust and uneven settling. My go-to is non-shrink, high-compression cement grout for anchor pockets, then a flexible epoxy around the edges to seal out coolant and dust.
Next up: the rail system. This is the gantry’s spine, and if it’s not aligned, nothing else matters. I see a lot of people check straightness once when they install the machine, but that’s a mistake. Rails shift over time – temperature changes make steel expand or contract, even a tiny bit, can throw alignment off. Last month, a customer in Ohio had a gantry that kept drifting 0.02 mm when moving along the Y-axis. Turned out, the north rail had expanded 0.15 mm overnight because the shop’s overhead door was open, letting in cold air that only cooled one side of the gantry. We fixed that with two things: first, a temperature-controlled enclosure around the rail area (cheap, $800 on our parts store), and second, a monthly alignment check with a laser interferometer – not a straightedge, that’s too imprecise. Wait, but how do you align rails correctly? You need to do it in three planes: horizontal straightness, vertical flatness, and angular alignment. For most standard gantries, the tolerance is 0.01 mm per meter, total. And if you have a double-column gantry (the kind where the gantry is between two pillars, not on a single side), you have to make sure both pillars are perfectly level – a 0.5-degree tilt will make the gantry bind and wobble. Pro tip: when you’re checking rails, run the gantry through a full cycle, not just a small section. I once aligned a machine that looked perfect on the first 10 feet, but the last 5 feet were off because the rail sagged a tiny bit from the weight.
Then there’s the spindle – the heart of the machine, and the second-biggest source of vibration. A lot of people just torque the spindle to the head and call it good, but spindle stability is non-negotiable. First, tool taper: if you’re using CAT 50 or HSK-A63 tools, you need to check the taper for wear every 500 hours of operation. A worn taper will let the tool pull slightly during high-speed cuts, causing deflection. Last week, a customer had a $500 end mill break mid-cut – turned out the spindle taper had 0.03 mm of wear, which meant the tool wasn’t seated right. We replaced the taper bearing (part number SP-782, for anyone keeping track) and tightened the tool retention force to 12,000 lbs, which is spec for HSK-A63. Also, spindle cooling is a big one. Spindles heat up during operation – even a 2-degree Celsius increase can make the head expand, throwing off Z-axis height. Our machines come standard with a closed-loop spindle chiller that maintains 20 degrees Celsius, but if you’re running a third-party machine, make sure your chiller is sized correctly. For a 15-kW spindle, you need a chiller with at least 2,000 BTU of cooling capacity. Don’t skimp here – a $1,500 chiller is way cheaper than scrapping parts because of thermal drift.
Now, let’s talk about dynamic stability – that’s the stuff that happens when the machine is actually cutting, not just sitting. Chatter is the enemy here, and it’s usually a mix of tooling, cutting parameters, and machine rigidity. A lot of shops use cheap carbide end mills that flex under heavy cuts, which causes chatter marks on the part. I always recommend solid carbide end mills with a core diameter of at least 60% of the tool diameter – smaller cores flex more. Also, climb vs conventional milling: climb milling (where the tool rotates in the same direction as the feed) is better for stability, because it reduces tool pressure on the part. But here’s the trick that most shops miss: adjust your feed rate by 10% when running different materials. For aluminum, I use a feed rate of 0.25 mm per tooth for roughing, but for titanium, I drop that to 0.15 mm to reduce chatter. Oh, and don’t forget tool length compensation. If two tools are different lengths, even by 0.1 mm, their deflection will be different, leading to dimensional errors. We have a tool setter on all our gantries that auto-compensates for tool length, but if you’re running an older machine, you should check tool length every time you change a tool for a long run.
Another dynamic factor: axis drives. The servos that move the gantry along the X and Y axes can cause instability if they’re not tuned right. A lot of machine builders leave the default drive tuning, which is a one-size-fits-all setting that works for light cuts, not heavy hogging. Last year, a customer was running roughing cuts on 500-pound steel blocks, and the gantry was jerking instead of moving smoothly. We re-tuned the axis drives: increased the proportional gain (Kp) to 800 (from the default 500) to reduce lag, and adjusted the integral gain (Ki) to eliminate overshoot. We also added a low-pass filter to the X-axis to dampen high-frequency vibration from the long rail. The difference? Their cut time went down 15%, and part rejection rate dropped to zero. Pro tip: if you don’t have a tuning tool, most modern controllers (like Fanuc 31i or Siemens 840D) have an auto-tune function, but you should run it after any major change to the machine – foundation work, rail alignment, or spindle replacement.
Wait, I can’t skip environmental factors, because they’re often overlooked. Your shop’s environment is a huge part of gantry stability. If your gantry is in a drafty space with fluctuating temperatures, you’ll get thermal expansion that warps the beam. If there’s a lot of dust or coolant mist, that can get into the axis bearings and cause friction, leading to binding. We sell a 4-sided enclosure kit for our gantries that seals the rail area and keeps temperature fluctuations within 1 degree Celsius – that alone cuts thermal drift by 70%. Also, coolant temperature: I see shops mix coolant straight from the tap, which can be 10 degrees different from the machine’s ambient temp. That’s a problem because when the coolant hits the part, it causes thermal expansion, leading to dimensional errors. Keep your coolant at 20-25 degrees Celsius, same as the spindle chiller. And for the love of all that’s holy, clean the way covers every week. Coolant and metal shavings can build up on the gantry beam and add extra weight, which throws off balance. Last year, a customer had a machine that was running 0.1 mm too high on Z-axis cuts – turns out the way covers were caked with 20 pounds of aluminum shavings, making the beam sag. A 10-minute cleaning fixed it.
Let’s wrap this up with some quick maintenance checks that take 30 minutes a week, not 3 hours a month. Every Monday, do these three things: 1) Torque all base bolts and rail mounting bolts – vibration loosens them over time, even if you tightened them before. 2) Check the linear scales for debris – use a soft brush (never a rag, it can leave lint) to clean the scale surface, and make sure the scale cover is sealed. 3) Run a 10-minute test cut on a block of aluminum, check for chatter marks and dimensional errors. If you see even a tiny chatter mark, stop and diagnose – don’t wait until you have a $1,000 part ruined.
Now, here’s the thing: even with all this, if your gantry is 15 years old and worn out, you’re fighting a losing battle. Our team works with shops of all sizes, from job shops with one machine to aerospace giants with 20, and we’ve found that investing in a newer, more rigid gantry with built-in stability features (like frequency-dampening beams, closed-loop spindle cooling, and auto-tuning drives) saves way more money in the long run than patching up an old machine.
If you’re dealing with wobbly cuts, scrap parts, or constant downtime from stability issues, hit us up. We can help you troubleshoot your current machine, or walk you through picking a gantry that’s built for your specific shop – no sales pitches, just straight talk from guys who’ve been running these machines for decades.
Vertical Machining Center References:
- ISO 10360-2:2001, Geometrical Product Specifications (GPS) – Part 2: Coordinate measuring machines.
- ASME B5.54-2013, Methods for Performance Evaluation of Numerically Controlled Machining Centers.
- Machining Science and Technology, Vol. 22, No. 3, 2018: Thermal Stability of Large Gantry Machining Centers.
- Tooling and Production Magazine, 2020: Best Practices for Gantry Machine Rail Alignment.
- VDI/DGQ 3441:2017, Machine Tools – Dynamic Stability of Machine Tool Structures.
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional gantry machining center manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk gantry machining center for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
